Quality assurance
Quality engineered into every cable
A submersible cable spends its life underwater, out of sight. That is why we check it at every stage — so it keeps working long after it is installed.
Our process
From raw material to finished cable
Five stages, each with its own checks, so every metre of cable performs consistently.
- 01
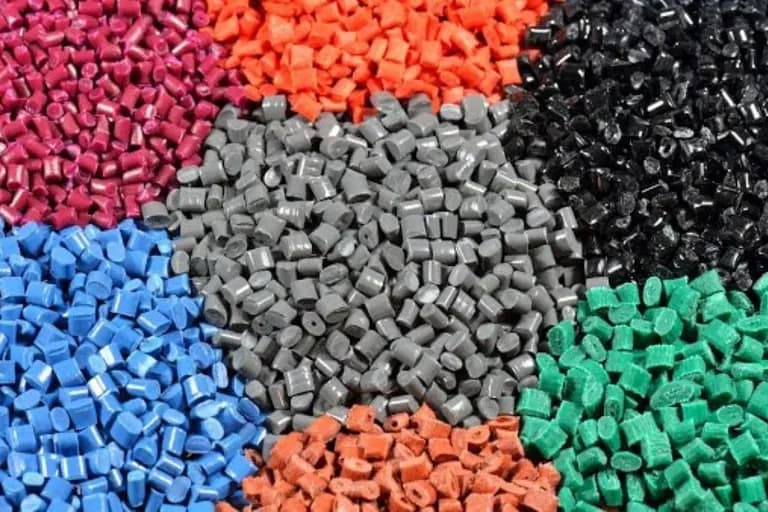
Raw material selection
Copper and PVC compound are selected for purity and consistency before production begins.
- 02
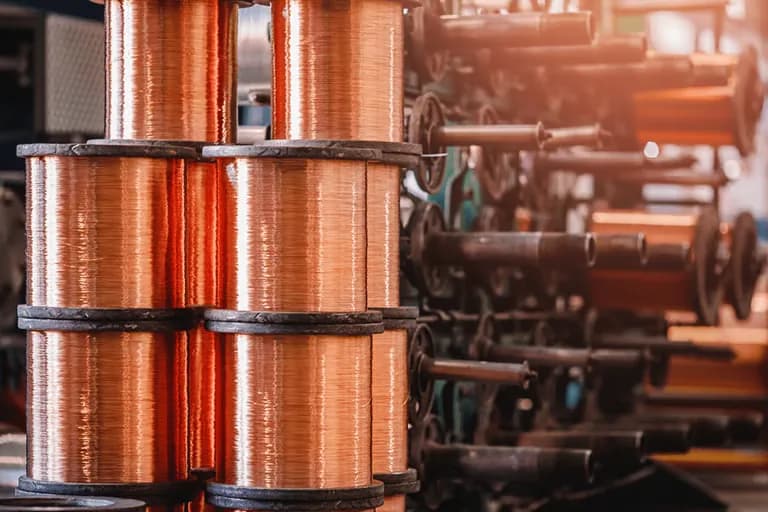
Conductor manufacturing
High-purity copper is drawn and stranded into flexible, uniform conductors.
- 03
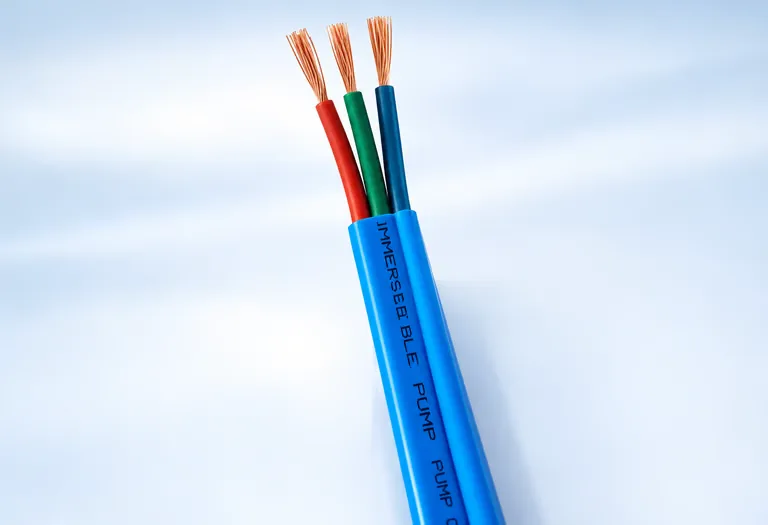
Insulation
Specially formulated PVC is applied to each core with uniform coverage and colour coding.
- 04
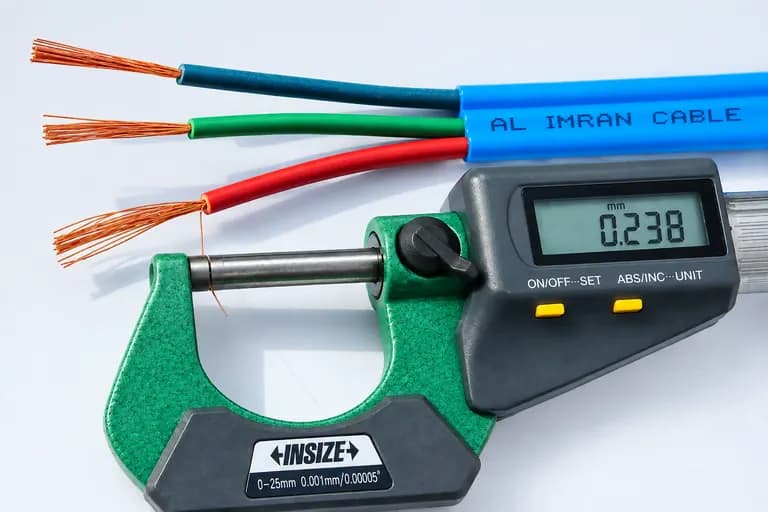
Production testing
Spark testing and in-process inspection catch pinholes and dimensional issues on the line.
- 05
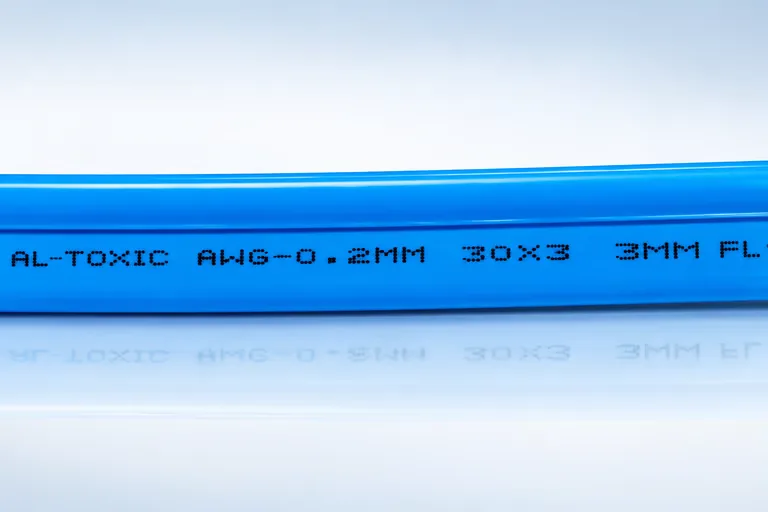
Finished cable testing
Final checks on the completed cable and its print marking before it is dispatched.
Spark testing
Finding defects you can't see
During production the insulated conductor passes through a high-voltage electrode. Any pinhole, microscopic defect or weak spot in the insulation causes a spark that is instantly detected — so the defect can be removed before the cable ever reaches a well.
Learn more in our article What is spark testing and why it matters.
Illustrative spark-test animation
What we check
Five promises in every metre
Spark Tested
High-voltage spark testing detects pinholes, microscopic defects and insulation weaknesses during production.
Uniform Insulation
Consistent insulation coverage around every core lowers the risk of failure in service.
Thermal Stability
Insulation formulated to hold up during continuous pump operation.
Moisture & Water Resistance
Engineered for wet environments and long-term submersion.
Consistent Performance
Checks from raw material to finished product so every metre performs like the last.
Quality you can specify with confidence.
Tell us your pump rating, well depth and cable length — our team will recommend the right AL IMRAN submersible cable and send you a quote.